Auto Repair Shop In Plainfield, IL

Why Choose a Chocolate Processing Plant?
Choosing a Chocolate Processing Plant can turn a promising recipe into a consistent commercial product. It brings roasting, refining, conching, tempering, molding, and cooling into one controlled workflow. Each stage affects flavor, texture, appearance, and shelf stability. A well-designed plant also reduces unnecessary handling. That matters.
In my experience, small process changes can create visible differences. A few degrees during tempering may cause dull surfaces or unwanted streaks. Poor particle refinement can leave chocolate feeling sandy. Reliable equipment helps production teams monitor temperature, viscosity, sanitation, and batch records more carefully. These controls support repeatable quality and stronger customer trust.
Dr. Carla D. Martin, executive director of the Fine Cacao and Chocolate Institute, has said, “Chocolate is a lens through which we can understand the world.” Her observation reaches beyond taste. A processing plant connects farmers, technicians, product developers, and consumers through measurable decisions. It can help manufacturers protect cocoa character while meeting practical production demands.
Still, a Chocolate Processing Plant is not a magic solution. Equipment requires skilled operators, preventive maintenance, responsible sourcing, and realistic capacity planning. Energy use and cleaning time also deserve honest attention. A larger factory may increase output, yet it can create waste when demand forecasts are weak. That is an uncomfortable possibility.
The best choice depends on product goals, batch size, available capital, and technical competence. Careful planning should come before impressive machinery. When those elements align, the plant becomes more than a production site. It becomes a dependable foundation for safe, efficient, and distinctive chocolate.
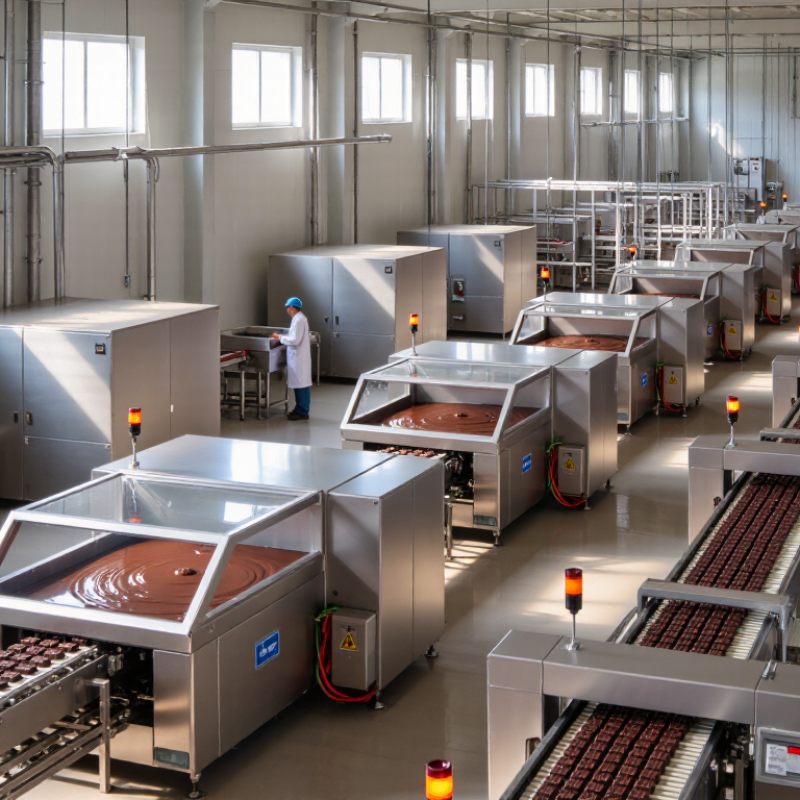
Why Choose a Chocolate Processing Plant?
Cocoa Bean Roasting at 120–140°C: Developing Flavor and Safety
A professional chocolate processing plant provides controlled roasting conditions for cocoa beans. At 120–140°C, heat reduces moisture and helps develop deeper cocoa aromas. The beans may release notes of nuts, caramel, toast, or dried fruit. Roasting time must match bean size, origin, moisture, and machine airflow. Temperature alone never tells the whole story.
Operators monitor the roast with calibrated probes and regular sensory checks. A clean, even batch should show consistent color and a crisp shell. Safe processing also requires documented sanitation, allergen controls, and validated time-temperature procedures. These practices reduce microbial risks without depending on guesswork. Small changes matter. A few extra minutes can create harsh, smoky flavors.
Experienced teams usually compare each batch with approved reference samples. They record inlet temperature, product temperature, roast duration, and cooling speed. Rapid cooling helps prevent residual heat from overdeveloping the flavor. Still, no roasting profile is perfect. Natural cocoa beans vary, and one setting may perform differently during humid weather. I have found that careful sampling often reveals problems before laboratory results do. That human check remains important, even in a highly automated plant.
| Processing Dimension | Typical Operating Range or Target | Effect on Cocoa Beans | Plant-Level Control Point |
|---|---|---|---|
| Roasting temperature | 120–140°C bean or air temperature | Promotes Maillard reactions, reduces raw or acidic notes, and develops chocolate, nutty, caramel, and roasted aromas. | Use calibrated temperature sensors and maintain a validated roast profile for each cocoa origin and bean size. |
| Roasting time | Commonly about 15–45 minutes, depending on equipment, batch size, bean size, and target flavor | Longer or more intense roasting generally produces darker roast notes but may reduce delicate origin aromas and create bitterness if excessive. | Control time together with temperature; temperature alone does not define the thermal treatment. |
| Bean moisture | Typically approximately 5–8% before roasting; the exact specification depends on raw-bean quality and plant standards | Moisture loss supports crispness and shell separation. Excessive moisture can extend roasting time and produce uneven flavor development. | Measure incoming moisture and verify final moisture to maintain consistent roasting and winnowing performance. |
| Flavor development | Profile selected according to origin, fermentation level, bean size, and desired chocolate style | Roasting transforms fermentation-derived precursors into aroma compounds associated with cocoa, toast, nuts, caramel, and dried fruit. | Combine sensory evaluation with color, aroma, moisture, and roast-loss records rather than relying on a single measurement. |
| Acidity and astringency | Reduced progressively as the roast becomes more intense | Moderate roasting can soften sharp acidity and astringency; excessive roasting may mask desirable origin character. | Set sensory limits for acidity, bitterness, and astringency for each product specification. |
| Microbial safety | A validated time–temperature process is required; 120–140°C is not, by itself, a universal safety guarantee | Roasting substantially reduces vegetative microorganisms when the required heat exposure reaches the coldest part of the product. | Validate the process using product-core temperature, residence time, airflow, load, and microbiological verification. |
| Uniformity of roasting | Consistent bean temperature and airflow throughout the batch | Uniform roasting minimizes under-roasted beans, burnt beans, uneven aroma, and inconsistent color. | Use controlled agitation, even loading, airflow monitoring, and routine sampling from different points in the batch. |
| Cooling after roasting | Rapid cooling immediately after the target roast is reached | Stops further roasting and protects the intended flavor, color, and aroma profile. | Verify cooling-air cleanliness and reduce bean temperature promptly before storage or grinding. |
| Quality verification | Batch records, sensory checks, moisture testing, color assessment, and food-safety monitoring | Provides evidence that flavor, safety, and process consistency meet the defined product specification. | Maintain traceable records for raw beans, roast profile, cooling, deviations, corrective actions, and release testing. |
Note: Actual roasting conditions vary by cocoa origin, fermentation, bean size, equipment design, batch load, and product requirements. Food-safety performance must be confirmed through a documented and validated process.
